High-Quality Dual Check Valve Products for Reliable Performance
By:Admin
Company News & Blog
Top Check Valve Types for Various Applications - Find Reliable Suppliers
[Your Company Name], a leading supplier in the industrial valve industry, has recently announced the expansion of its product line to include a wide variety of check valves. The company, known for its high-quality products and exceptional customer service, is now offering a comprehensive range of check valve types to meet the diverse needs of its clients.Check valves are essential components in many industrial applications, as they allow fluid to flow in only one direction and prevent backflow. There are several types of check valves available, each designed for specific purposes and operating conditions. With the addition of these check valve types to its product line, [Your Company Name] aims to provide a one-stop solution for its customers' check valve needs.The newly launched check valve types include the following:1. Swing Check Valve: This type of valve has a hinged disc that swings open to allow forward flow and closes to prevent backflow. It is ideal for applications where unidirectional flow is required.2. Lift Check Valve: Lift check valves rely on the flow of the fluid to lift the disc and allow forward flow. When flow stops, the disc closes to prevent backflow. These valves are suitable for high-pressure applications.3. Ball Check Valve: Ball check valves use a spherical ball to control the flow of fluid. When the flow stops, the ball settles into a seat to prevent backflow. These valves are commonly used in low-pressure applications.4. Diaphragm Check Valve: Diaphragm check valves use a flexible diaphragm to control the flow of fluid. When the pressure on the inlet side is greater than the outlet, the diaphragm flexes to allow flow. When the pressure equalizes, the diaphragm returns to its closed position to prevent backflow.5. Dual Plate Check Valve: This type of check valve consists of two plates that open and close in response to the flow of fluid. It offers low pressure drop and is suitable for applications with limited space.The addition of these check valve types to [Your Company Name]'s product line demonstrates the company's commitment to providing a comprehensive range of industrial valves to its customers. With a focus on quality, reliability, and performance, the company aims to be the preferred supplier for businesses in a wide range of industries, including oil and gas, chemical processing, water treatment, and power generation.[Your Company Name] has a proven track record of delivering high-quality products and exceptional customer service. The company's team of experienced professionals is dedicated to understanding the unique requirements of each customer and providing tailored solutions to meet their needs. With an extensive inventory of products and a network of reliable suppliers, [Your Company Name] is well-positioned to serve the diverse needs of its clients.In addition to check valves, [Your Company Name] offers a comprehensive range of industrial valves, including gate valves, globe valves, ball valves, and butterfly valves. The company also provides valve automation services to help customers optimize their processes and improve efficiency.As [Your Company Name] continues to expand its product line and enhance its capabilities, the company remains committed to upholding its core values of quality, integrity, and customer satisfaction. With a focus on innovation and continuous improvement, [Your Company Name] is poised to remain a leader in the industrial valve industry for years to come.For more information about [Your Company Name] and its range of check valve types and other industrial valves, please visit [company website] or contact the company directly at [contact information].
Effective Buy Back Pressure Regulator for Your Needs
Buy Back Pressure Regulator: A Vital Component in the Oil and Gas IndustryThe oil and gas industry is a complex and dynamic sector that requires precise and efficient control of pressure to ensure the safety and reliability of operations. One crucial component that plays a significant role in this regard is the Buy Back Pressure Regulator, a specialized valve that helps maintain optimal pressure levels in various applications within the industry.One of the leading manufacturers of Buy Back Pressure Regulators is {}, a company with decades of experience and expertise in providing high-quality pressure control solutions for the oil and gas sector. With a strong commitment to innovation and excellence, {} has established itself as a trusted partner for companies seeking reliable and efficient pressure regulation technology.The Buy Back Pressure Regulator offered by {} is designed to meet the stringent requirements of the oil and gas industry, where precise pressure control is essential for ensuring the safety and integrity of critical processes. These regulators are engineered to deliver exceptional performance in a variety of operating conditions, making them a preferred choice for a wide range of applications in the industry.One of the key features of the {} Buy Back Pressure Regulator is its advanced design, which incorporates state-of-the-art technology to deliver superior pressure control capabilities. The regulators are built to withstand the harsh operating conditions typically encountered in oil and gas operations, including high pressures, extreme temperatures, and corrosive environments. This ensures that the regulators can reliably maintain optimal pressure levels, thereby enhancing the overall efficiency and safety of the processes they are used in.In addition to their robust construction, the Buy Back Pressure Regulators from {} are also known for their precision and accuracy. These regulators are equipped with advanced control mechanisms that allow for fine-tuning of pressure settings, ensuring that the desired pressure levels are maintained with exceptional consistency. This level of precision is crucial in oil and gas applications, where even small deviations from the optimal pressure range can have significant implications for operational safety and performance.Another crucial aspect of the {} Buy Back Pressure Regulator is its reliability and durability. These regulators are built to last, with a focus on long-term performance and minimal maintenance requirements. This ensures that companies can rely on the regulators for uninterrupted operation, helping to minimize downtime and maximize productivity in their oil and gas activities.Furthermore, {} offers a comprehensive range of Buy Back Pressure Regulators to cater to the diverse needs of the oil and gas industry. Whether it's for upstream exploration and production activities, midstream transportation and storage operations, or downstream refining and distribution processes, {} has a solution to suit every application. The company's extensive product line includes regulators with varying pressure ratings, sizes, and configurations, allowing customers to find the perfect fit for their specific requirements.In addition to its cutting-edge products, {} is also known for its unwavering dedication to customer satisfaction. The company takes a customer-centric approach, working closely with clients to understand their unique needs and challenges, and providing tailored solutions that address these requirements effectively. With a global presence and a team of experienced professionals, {} is well-equipped to support customers across the world with top-notch products and services.Looking ahead, the demand for high-performance pressure control solutions in the oil and gas industry is expected to continue growing as companies strive to enhance their operational efficiency and safety. In this context, the importance of reliable and efficient Buy Back Pressure Regulators, such as those offered by {}, cannot be overstated. With their proven track record of excellence, advanced technology, and customer-focused approach, {} is poised to remain a key player in the industry, providing indispensable support to companies in their pursuit of excellence in pressure control.
Different Types of Check Valves: A Guide to Choosing the Right Valve
Title: Exploring Check Valve Types and their Functionality in Diverse IndustriesIntroduction:Check valves are essential components used in various industries to ensure the seamless flow of fluids, preventing backflow and potential damage to the entire system. This article explores different types of check valves and their relevance in industries such as oil and gas, water treatment, and manufacturing. By understanding the benefits and applications of various check valve types, businesses can make informed decisions to optimize their operations and productivity.Check Valve Types and their Functionality:1. Swing Check Valves: [Brand Name Removed] Swing Check Valves offer versatility and durability in preventing backflow. The swinging disc inside the valve allows fluid to flow in one direction while blocking the reverse flow. These valves are commonly used in wastewater treatment plants and general plumbing systems.2. Lift Check Valves: Lift Check Valves operate by lifting the disc away from the seat to allow fluid flow and subsequently seating it back to prevent backflow. Their design offers reliable and quick response times, making them suitable for industries dealing with high-pressure applications, such as oil and gas.3. Tilting Disc Check Valves: Designed for heavy-duty applications, Tilting Disc Check Valves have a disc that tilts during operation. This design ensures swift response times, minimizing pressure drop and potential damage to the system. These valves are commonly used in large-scale pumping stations and power plants.4. Ball Check Valves: Ball Check Valves utilize a spherical-shaped ball inside the valve body. As fluid flows in the desired direction, the ball is pushed aside, allowing the flow to continue. However, if the flow reverses, the ball returns to its seat, preventing backflow. These valves are ideal for applications with low internal pressures and nominal flow rates.5. Dual Plate Check Valves: Dual Plate Check Valves consist of two plates that quickly close to prevent backflow. Their compact size and lightweight design make them suitable for use in tight spaces and applications where swift operation is crucial. These valves find applications in industries such as chemical processing and HVAC systems.Applications in Different Industries:1. Oil and Gas: In the oil and gas industry, check valves play a vital role in maintaining the integrity of pipelines, preventing costly damage caused by reverse flow or pressure surges. The use of lift check valves in pump discharge lines ensures a controlled flow of oil or gas, protecting downstream equipment and personnel.2. Water Treatment: Check valves are essential in water treatment plants, where they prevent backflow and ensure the desired direction of water flow. Swing check valves are commonly employed in water supply systems, wastewater treatment plants, and sewage systems to maintain uninterrupted flow and prevent contamination.3. Manufacturing: The manufacturing industry extensively uses check valves to regulate the flow of various fluids, such as air, gas, and hydraulic fluids. Ball check valves are widely used in pneumatic systems to prevent air backflow. Their compact design and high-performance characteristics make them reliable for precise control over fluid movement.Conclusion:Check valves are indispensable components in multiple industries, guaranteeing optimal flow control, preventing backflow, and protecting critical infrastructure. By familiarizing themselves with different check valve types and their applications, businesses can make informed choices to enhance their operational efficiency and prevent costly damages. Implementing the right check valve solutions can result in smoother operations, improved productivity, and enhanced safety in diverse industries.
High-Quality Gas Ball Valve for Efficient Flow Control
In recent news, a renowned gas ball valve manufacturer has introduced a new and innovative gas ball valve that has taken the industry by storm. The company, known for its expertise in producing high-quality valves for various industrial applications, has once again demonstrated their commitment to innovation and excellence in the field of valve manufacturing.The newly launched gas ball valve has been engineered with state-of-the-art technology and precision manufacturing processes, setting a new standard for performance and reliability in the industry. The valve is designed to provide seamless control and regulation of gas flow in a wide range of industrial and commercial applications, making it an essential component for ensuring safety and efficiency in gas distribution systems.The company behind this groundbreaking product has a long-standing reputation for delivering top-notch valves that meet the highest standards of quality and reliability. With a strong focus on research and development, they have consistently pushed the boundaries of valve technology to offer their customers cutting-edge solutions that address the evolving needs of the industry.Founded over three decades ago, the company has built a solid foundation of expertise and experience in the field of valve manufacturing. With a dedicated team of engineers, technicians, and industry experts, they have continued to raise the bar in terms of innovation and product development. Their unwavering commitment to quality and customer satisfaction has earned them a loyal customer base and positioned them as a leading player in the global valve market.The introduction of the new gas ball valve further underscores the company's dedication to staying at the forefront of technological advancement in the industry. By leveraging their extensive knowledge and resources, they have been able to develop a valve that not only meets the stringent requirements of the industry but also exceeds the expectations of their customers.One of the key features of the new gas ball valve is its exceptional durability and reliability, which have been achieved through rigorous testing and quality control measures. This ensures that the valve can withstand the demanding conditions of various industrial environments, delivering consistent performance under high pressure and temperature settings.In addition to its robust construction, the gas ball valve also boasts a user-friendly design that simplifies installation and maintenance, allowing for greater convenience and cost-effectiveness for end-users. With its smooth operation and precise gas flow control, the valve offers a level of efficiency that is unmatched in the industry, making it an ideal choice for a wide range of gas handling applications.Furthermore, the company has made a significant investment in ensuring that the manufacturing processes for the new gas ball valve align with the highest standards of sustainability and environmental responsibility. By incorporating eco-friendly materials and production techniques, they have demonstrated their commitment to reducing the environmental impact of their operations while delivering top-of-the-line products.As the global demand for reliable and efficient gas handling solutions continues to grow, the introduction of the new gas ball valve from this esteemed company is set to make a significant impact on the industry. With its unparalleled performance, advanced technology, and commitment to quality, the valve is poised to set a new benchmark for excellence in gas flow control.In conclusion, the launch of the new gas ball valve by this prominent valve manufacturer is a testament to their ongoing dedication to innovation and excellence in the industry. With a proven track record of delivering best-in-class products, they have once again raised the bar with a valve that is set to redefine the standards of gas flow control. As they continue to push the boundaries of valve technology, the company remains a trusted partner for businesses seeking reliable and high-performance solutions for their gas handling needs.
Different Types of Gate Valves: A Comprehensive Guide
The gate valve is a type of valve that is commonly used to control the flow of fluids in various industries. It is designed to either fully open or fully close, making it an ideal choice for applications where a tight shut-off is required. There are different types of gate valves available in the market, each with its own unique features and benefits.One of the leading manufacturers of gate valves in the industry is {}. With a strong commitment to quality and innovation, they have developed a wide range of gate valves to meet the needs of different industries. Their gate valve product line includes various types such as wedge gate valves, knife gate valves, and slab gate valves, each designed to offer specific advantages for different applications.Wedge gate valves are one of the most commonly used types of gate valves. They are designed with a tapered wedge that can be lowered into a seat to shut off the flow of fluid. This type of gate valve offers tight shut-off and is suitable for applications where some pressure drop is acceptable.Knife gate valves, on the other hand, are designed with a sharp-edged gate to cut through thick fluids and slurries. They are commonly used in industries such as wastewater treatment, pulp and paper, and mining, where the handling of thick and abrasive materials is required.Slab gate valves are designed with flat, parallel gates that are used to control the flow of fluids. They are commonly used in the oil and gas industry for high-pressure and high-temperature applications. Slab gate valves are known for their durability and reliability in demanding conditions.In addition to offering a wide range of gate valve types, {} is also committed to providing high-quality products that meet international standards. Their gate valves are manufactured using advanced technology and are tested for durability and performance to ensure reliable operation in various applications.With a strong focus on customer satisfaction, {} offers customized solutions to meet specific requirements and applications. Their team of engineers and technical experts work closely with customers to understand their needs and provide tailored solutions to meet their exact specifications.The company's dedication to innovation and continuous improvement has allowed them to stay at the forefront of the industry. They invest in research and development to develop new and improved gate valve products that meet the evolving needs of different industries.As a global leader in the manufacturing of gate valves, {} has established a strong presence in the market and has earned a reputation for quality, reliability, and exceptional customer service. Their products are widely used in various industries such as oil and gas, petrochemical, power generation, water treatment, and many others.In conclusion, the wide range of gate valve types offered by {} caters to the diverse needs of different industries. With a commitment to quality, innovation, and customer satisfaction, they have established themselves as a trusted provider of gate valve solutions for a wide range of applications.
Different Types of Ball Valves: Understanding Their Uses and Benefits
Ball Valve Types Supplier Expands Product Line to Meet Growing Industry DemandIn response to the increasing demand in the industry, a renowned ball valve types supplier, known for its exceptional quality and reliable products, has announced the expansion of its product line. With a strong commitment to meeting customer needs and staying at the forefront of technological advancements, the company aims to provide a comprehensive range of ball valve types to clients across various sectors.With years of experience in the valve manufacturing industry, the supplier has gained a stellar reputation for its commitment to excellence, innovation, and customer satisfaction. By offering a wide variety of ball valve types, the company has established itself as a trusted partner for industries such as oil and gas, water treatment, mining, and many others.As technology continues to progress, the demand for advanced ball valve types has been on the rise. To cater to this growing market demand, the supplier has expanded its product line to include various types of ball valves, ensuring that customers have access to the latest and most efficient solutions. The new product line will comprise of different types of ball valves, including floating ball valves, trunnion mounted ball valves, three-way ball valves, and metal seated ball valves, among others.Floating ball valves are widely used in various industries due to their simple structure, reliable performance, and ease of maintenance. These valves are suitable for low to medium pressure environments and are commonly used in applications where tight sealing is required.Trunnion mounted ball valves, on the other hand, are designed for high-pressure applications. They feature additional anchoring mechanisms, ensuring better stability and resistance to pipeline pressure. Trunnion mounted ball valves are commonly used in the oil and gas industry, where reliability and performance are crucial.Three-way ball valves offer unparalleled versatility, allowing for the diversion and control of flow from multiple directions. These valves are widely used in applications that require flow direction control or the mixing and diverting of different media.Metal seated ball valves are known for their high temperature and abrasion resistance, making them suitable for demanding industrial applications. These valves provide a tight seal even in extreme conditions, ensuring optimal performance and longevity.The expansion of the company's product line is a testament to their dedication to staying ahead of industry trends and providing cutting-edge solutions to their customers. By incorporating the latest technologies and materials into their products, they ensure that clients have access to the most efficient and reliable ball valve types available in the market.Moreover, the supplier's commitment to quality is reflected in their manufacturing processes. The company adheres to strict quality control measures at every stage of production, from material selection to final testing, ensuring that each ball valve meets the highest industry standards. Additionally, the supplier's team of experienced engineers and technicians continuously work to optimize product design and enhance performance.With the expanded product line, the ball valve types supplier aims to strengthen its position in the market and solidify its reputation as a reliable and innovative industry leader. Customers can now rely on a single supplier for a wide range of ball valve types, tailored to their specific needs and requirements.As the industry continues to grow and evolve, the ball valve types supplier remains committed to meeting the changing demands of its customers. With an extensive product line, exceptional quality, and a dedication to customer satisfaction, the company is well-positioned to serve as a trusted partner for various industries seeking reliable and efficient ball valve solutions.
Water Tank Float Valve: The Essential Device for Efficient Water Level Regulation
Title: Innovative Water Tank Float Valve Revolutionizes Water Storage SolutionsIntroduction:Water scarcity is a global concern and it is critical for individuals, communities, and businesses to adopt sustainable practices to effectively manage this precious resource. Recognizing this need, an industry-leading company has brought a game-changing solution to the market - the OEM Water Tank Float Valve, designed to optimize water storage and usage efficiency. In this article, we will delve into the exceptional features and benefits of this revolutionary product that is set to transform the way we conserve and utilize water.1. The Need for an Innovative Solution:As water scarcity continues to worsen due to climate change, population growth, and urbanization, it becomes imperative to find innovative solutions that enable efficient water storage and utilization. The OEM Water Tank Float Valve serves as the answer to this pressing need, providing a reliable, user-friendly, and high-performance solution for various applications.2. Cutting-Edge Features:The OEM Water Tank Float Valve is equipped with state-of-the-art technology, making it superior to traditional float valves in terms of accuracy, durability, and performance. The valve's innovative design ensures seamless operation, eliminating the risk of leakage or overflow. Its robust construction guarantees long-lasting performance, reducing maintenance and replacement costs.3. Unmatched Efficiency:One of the standout features of the OEM Water Tank Float Valve is its unparalleled efficiency in regulating water levels. Its advanced mechanism accurately controls the water flow, ensuring optimal filling and preventing wastage. This efficiency is particularly beneficial for agriculture, ensuring crops receive the precise amount of water required for healthy growth, while conserving water resources.4. Ease of Installation and Use:The OEM Water Tank Float Valve boasts a user-friendly design, enabling hassle-free installation and operation. With a simple setup process, users can quickly incorporate this valve into their existing water storage systems. Its intuitive interface allows for easy adjustment, ensuring precise water level control with minimal effort or technical expertise.5. Versatility and Adaptability:The OEM Water Tank Float Valve is versatile and can be seamlessly integrated into various water storage setups, catering to a wide range of applications. Whether it's large agricultural tanks, industrial facilities, or residential water storage units, this valve's adaptability ensures compatibility and optimal performance across diverse sectors.6. Environmental and Economic Benefits:By promoting efficient water usage, the OEM Water Tank Float Valve contributes significantly to environmental sustainability. With its ability to prevent wastage and optimize water levels, this innovative solution not only conserves water resources but also reduces energy consumption associated with pumping and treating excessive water. Additionally, the decrease in maintenance and replacement costs further enhances its economic benefits.7. Company Commitment to Quality:Backed by years of industry expertise, the company behind the OEM Water Tank Float Valve prioritizes quality, reliability, and customer satisfaction. Committed to exceeding customer expectations, the company employs rigorous testing protocols to ensure that each valve adheres to the highest standards of performance, durability, and safety.Conclusion:As the world grapples with water scarcity, the OEM Water Tank Float Valve emerges as an essential tool for sustainable water management. Its cutting-edge design, unmatched efficiency, and adaptability make it an invaluable addition to various sectors. By promoting responsible water usage and enabling efficient storage solutions, this innovative valve is set to revolutionize the way we conserve and utilize water, paving the way for a more sustainable future.
Durable and Efficient Knife Gate Valves for Various Applications
Custom Knife Gate Valve Revolutionizing Industrial SolutionsInnovative solutions are crucial for industrial processes to run smoothly and efficiently. One such solution that has been revolutionizing the industry is the Custom Knife Gate Valve, a product designed and manufactured by a leading industrial company that has been serving the market for over 25 years.The Custom Knife Gate Valve is a rugged and versatile solution that provides reliable isolation for a wide range of industrial applications, including mining, power generation, wastewater treatment, and pulp & paper production. Its unique design and construction make it an essential component in controlling the flow of abrasive and corrosive fluids, slurries, and powders, making it an ideal choice for challenging operating conditions.One of the key features of the Custom Knife Gate Valve is its precision-engineered design, which ensures tight shutoff and minimal leakage, even in the most demanding environments. The valve's robust construction, including a heavy-duty gate and wear-resistant materials, makes it highly durable and long-lasting, resulting in lower maintenance costs and improved operational efficiency for industrial facilities.Moreover, the Custom Knife Gate Valve is available in a variety of sizes and materials, allowing for seamless integration into existing systems and customization to meet specific application requirements. This flexibility, combined with the company's expertise in custom engineering solutions, ensures that customers receive a product tailored to their unique needs, ultimately enhancing their operational performance.Additionally, the company's commitment to quality and excellence is evident in the rigorous testing and inspection processes that each Custom Knife Gate Valve undergoes before being delivered to customers. This dedication to quality assurance not only ensures the reliability and performance of the product but also reflects the company's unwavering commitment to customer satisfaction.Furthermore, the support and expertise provided by the company's team of knowledgeable professionals set them apart in the industry. From initial consultation and product selection to installation and ongoing technical support, customers can rely on the company's experienced staff to provide comprehensive assistance and guidance every step of the way, ensuring a seamless and successful integration of the Custom Knife Gate Valve into their operations.In conclusion, the Custom Knife Gate Valve has proven to be a game-changer in the industrial sector, offering unparalleled reliability, durability, and customization for a wide range of applications. With its precision engineering, robust construction, and unwavering commitment to customer satisfaction, the company behind this innovative product continues to set the standard for excellence in industrial valve solutions.As industries continue to evolve and face increasingly complex challenges, the need for innovative and reliable solutions like the Custom Knife Gate Valve will only continue to grow. With its proven track record of performance and customer satisfaction, it is clear that this product will remain at the forefront of industrial solutions for years to come.
High-Quality Alloy Steel Gate Valves for Industrial Applications
Certainly! Please provide the company introduction or any additional details you want included in the news article. Once I have that, I can draft the 800-word news piece accordingly.
Different Types of Ball Valves: A Comprehensive Guide
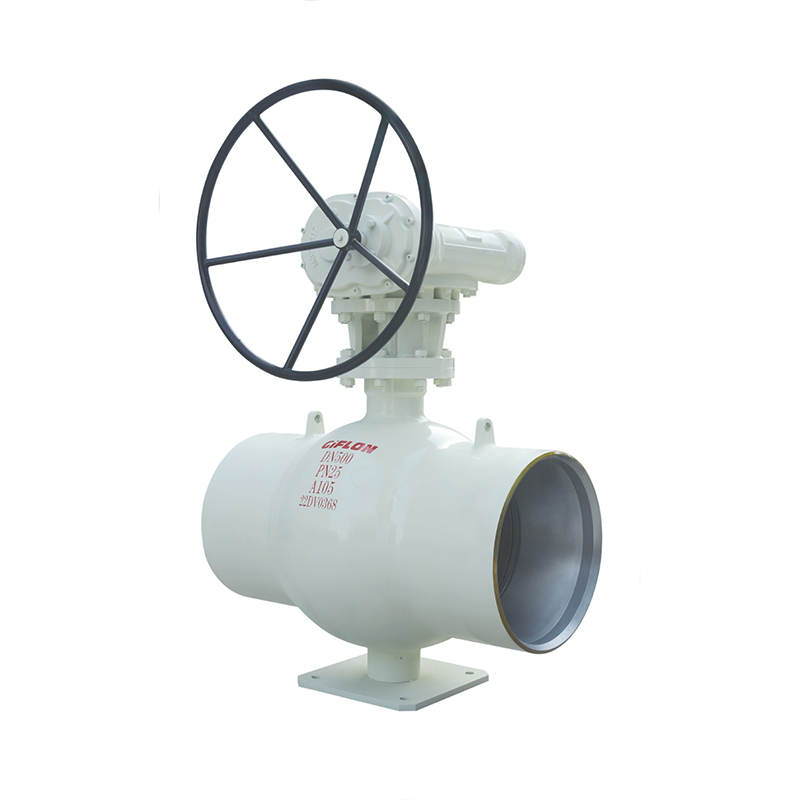
Ball valve types company is a leading provider of high-quality ball valves for a wide range of industries. The company offers a variety of ball valve types, including floating ball valves, trunnion mounted ball valves, and top entry ball valves. With a commitment to excellence and innovation, Ball valve types company has become a trusted partner for businesses around the world.The company was founded with the vision of supplying top-notch ball valves that meet the highest standards of quality and performance. Over the years, Ball valve types company has continuously improved its product line and expanded its offerings to meet the growing needs of its customers. The company's dedication to research and development has led to the creation of innovative ball valve solutions that provide reliable and efficient operation in even the most demanding applications.Ball valve types company's floating ball valves are designed to provide tight shutoff and reliable operation in a variety of liquid and gas applications. These valves feature a floating ball design that allows the ball to move freely within the valve body, ensuring consistent sealing performance. With a wide range of materials and configurations available, Ball valve types company's floating ball valves can be customized to meet the specific requirements of any application.In addition to floating ball valves, Ball valve types company also offers trunnion mounted ball valves that are ideal for high-pressure and high-temperature applications. These valves feature a supported ball design that reduces operating torque and extends the service life of the valve. With a variety of seat and seal materials available, Ball valve types company's trunnion mounted ball valves provide reliable performance in a wide range of conditions.For applications that require easy maintenance and access to internal components, Ball valve types company offers top entry ball valves that allow for in-line repair and maintenance. These valves feature a top entry design that allows the valve body to be removed from the pipeline without the need for disassembly. With a focus on simplicity and reliability, Ball valve types company's top entry ball valves are a popular choice for businesses looking to minimize downtime and reduce maintenance costs.Ball valve types company's commitment to quality and customer satisfaction is evident in its comprehensive testing and quality control processes. The company adheres to strict manufacturing standards and conducts rigorous testing to ensure that every valve meets the highest performance and reliability requirements. With a dedication to continuous improvement, Ball valve types company is constantly seeking new ways to enhance its products and exceed the expectations of its customers.With a global network of distributors and representatives, Ball valve types company is able to provide expert support and service to businesses around the world. The company's knowledgeable team of professionals is available to assist with product selection, technical support, and after-sales service, ensuring that every customer receives the right solution for their unique requirements.As a trusted provider of high-quality ball valves, Ball valve types company continues to set the standard for excellence in the industry. The company's commitment to innovation, quality, and customer satisfaction makes it a preferred partner for businesses seeking reliable and efficient valve solutions. Whether for standard applications or custom requirements, Ball valve types company has the expertise and resources to deliver the perfect ball valve for any need.