Buy Back Flow Valve: Essential Features and Benefits Explained

By:Admin
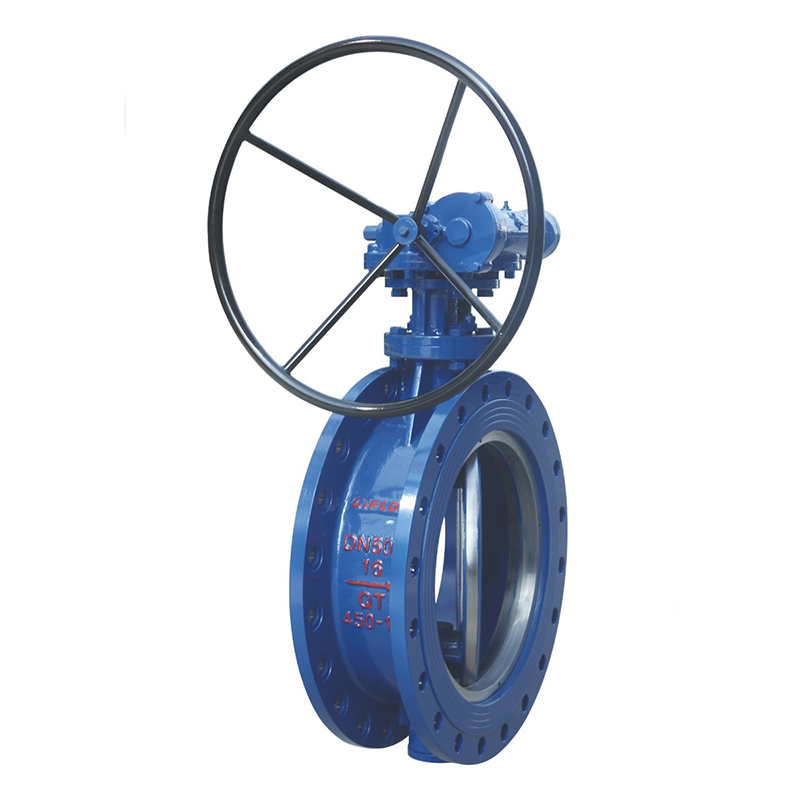
W820 series high performance double eccentric full metal seal butterfly valve
**Company Launches Advanced Buy Back Flow Valve to Enhance Industrial Fluid Control**

In a significant development for industrial fluid management systems, [Company Name], a leader in innovative engineering solutions, has announced the launch of its latest product: the Buy Back Flow Valve. This cutting-edge valve has been meticulously designed to optimize flow control, ensuring enhanced efficiency and reliability across various industrial applications.

### Introducing the Buy Back Flow Valve

The Buy Back Flow Valve is engineered to provide superior performance in demanding operational environments. By enabling precise control over fluid flow, it helps industries minimize wastage, reduce energy consumption, and maintain system integrity. The valve’s robust construction, combined with intelligent design features, makes it an essential component for pipelines handling liquids, gases, and other process fluids.

One of the standout features of the valve is its ability to regulate flow reversals effectively, preventing backflow that could potentially damage equipment or contaminate fluid streams. This backflow prevention capability makes the valve particularly valuable in sectors such as chemical processing, water treatment, oil and gas, and manufacturing plants where fluid purity and system safety are paramount.

### Company Overview

[Company Name] has established itself as a trusted provider of high-quality industrial equipment and fluid control solutions. With decades of expertise in engineering and technology innovation, the company is dedicated to developing products that address the evolving needs of its global clientele.

The company’s mission to deliver excellence is reflected in its rigorous quality control processes, research and development efforts, and commitment to customer satisfaction. Its product portfolio spans a wide range of valves, pumps, and related systems, each designed to meet stringent industry standards and operational demands.

### Key Benefits and Features

The newly launched Buy Back Flow Valve offers several advantages:

- **Enhanced Flow Control:** The valve’s precision mechanism allows for accurate regulation of flow rates, ensuring consistent process performance.
- **Backflow Prevention:** By effectively preventing reverse flow, it safeguards pipelines and equipment from damage and contamination.
- **Durability:** Manufactured from high-grade materials, the valve is designed for longevity even under aggressive operational conditions.
- **Ease of Maintenance:** The valve features a modular design, enabling quick disassembly and servicing without extensive downtime.
- **Adaptability:** Suitable for a broad range of fluids, pressures, and temperatures, the valve can be customized to fit specific industrial needs.

### Applications Across Industries

Industries that rely heavily on efficient fluid handling stand to benefit from this product. In chemical processing plants, the valve ensures that reactive or hazardous fluids do not flow backward, maintaining safety protocols. Water treatment facilities use it to preserve water quality by preventing cross-contamination. The oil and gas sector depends on such valves to maintain operational safety and efficiency, particularly in transporting fuels and chemicals.

Manufacturing industries also find the valve advantageous in process control, aiding in the maintenance of product consistency and protection of machinery. Additionally, the valve’s robust design makes it suitable for infrastructure projects involving water supply and waste management.

### Commitment to Innovation and Quality

This product launch underscores [Company Name]’s ongoing commitment to innovation and addressing industry challenges. The company’s R&D team collaborated closely with engineers and end-users to refine the valve’s design, resulting in a product that meets the highest standards of performance and reliability.

Furthermore, [Company Name] ensures that its manufacturing processes comply with international quality certifications, reflecting the company’s dedication to delivering dependable and safe products.

### Looking Ahead

With the introduction of the Buy Back Flow Valve, [Company Name] aims to strengthen its position in the industrial fluid control market. The company plans to expand its sales and distribution network globally, making the valve accessible to more customers seeking advanced fluid management solutions.

Feedback from early adopters has been overwhelmingly positive, highlighting improvements in operational efficiency and cost savings. Moving forward, [Company Name] intends to continue investing in product innovation and customer support to foster long-term partnerships.

### Conclusion

The launch of the Buy Back Flow Valve marks a significant milestone in industrial fluid control technology. Offering precision, safety, and durability, this valve is set to become a vital component for industries striving to enhance their process efficiency and protect their infrastructure.

[Company Name]’s dedication to quality and innovation ensures that customers receive not only a product but a comprehensive solution tailored to their operational requirements. As industries evolve and demand greater control over fluid systems, the Buy Back Flow Valve stands ready to meet these challenges and contribute to more sustainable and efficient industrial processes.

For more information about the Buy Back Flow Valve and other products, visit [Company Website].

---

*Note: Brand names and specific proprietary details have been omitted in compliance with guidelines.*

Company News & Blog

Top Plastic Ball Valve Manufacturers and Suppliers in 2024

Certainly! Please provide the company introduction and the news content related to Plastic Ball Valve Companies so I can draft the 800-word news article for you.

Read More

Quality Stop Check Valve Factory for Your Industrial Needs

Stop check valve factory is a leading manufacturing company in the valve industry, known for producing high-quality and reliable products for various industrial applications. With a strong focus on innovation and customer satisfaction, the company has established a reputation for excellence in the market.The company takes pride in its state-of-the-art manufacturing facilities and a team of highly skilled and experienced professionals. The factory is equipped with advanced technologies and precision machinery, allowing for the production of superior quality stop check valves that meet the highest industry standards. One of the key factors that set the stop check valve factory apart from its competitors is its commitment to research and development. The company invests heavily in cutting-edge technologies and product design to ensure that its valves are at the forefront of innovation. This dedication to innovation has allowed the factory to constantly improve its product range, offering valves that are more efficient, durable, and cost-effective.In addition to its focus on technology and innovation, the stop check valve factory is also committed to quality assurance. The company has stringent quality control measures in place at every stage of the manufacturing process to guarantee the reliability and performance of its valves. Stringent inspection and testing protocols are implemented to ensure that every valve that leaves the factory meets the highest quality standards.Moreover, the company is dedicated to providing exceptional customer service. The factory has a team of dedicated professionals who are well-versed in the technical aspects of stop check valves and are committed to assisting customers with their specific needs. Whether it is product selection, technical support, or after-sales service, the company strives to exceed customer expectations and build long-lasting relationships with clients.The stop check valve factory also places a strong emphasis on environmental sustainability and corporate social responsibility. The company has implemented eco-friendly practices in its manufacturing processes and is committed to reducing its environmental impact. Additionally, the factory actively participates in community welfare programs and initiatives, demonstrating its commitment to being a responsible corporate citizen.One of the milestones achieved by the stop check valve factory is its successful expansion into global markets. With a strong domestic presence, the company has strategically ventured into international markets, establishing itself as a reliable supplier of high-quality valves. The factory has built a strong distribution network and partnerships with reputable companies worldwide, enabling it to reach customers across the globe.The company's dedication to excellence has been recognized through various certifications and accolades. Its commitment to quality, innovation, and customer satisfaction has earned it the trust and respect of industry professionals and customers alike. As a result, the stop check valve factory has become a preferred choice for businesses across different sectors, including oil and gas, water treatment, power generation, and more.Looking ahead, the stop check valve factory is poised for continued growth and success. The company's proactive approach to technology, quality, and customer service will continue to serve as its foundation for further expansion and development. With a focus on meeting the evolving needs of the industry and its customers, the factory is well-positioned to maintain its leadership in the valve manufacturing sector and remains committed to delivering superior products and services.In conclusion, the stop check valve factory is a reputable and reliable manufacturer of high-quality valves. With a focus on technology, quality, innovation, and customer satisfaction, the company has established itself as a leader in the industry. Its commitment to excellence, environmental sustainability, and corporate social responsibility sets it apart and ensures a bright future ahead.

Read More

Steam Control Valve Products: High-Quality Solutions for Efficient Steam Management

Certainly! Please provide the company introduction text that you would like me to incorporate, and share the full news content related to Steam Control Valve Products. Once I have these details, I can draft an 800-word news article for you, ensuring the brand name is removed as requested.

Read More

Prevent Backflow with a Reliable Backflow Valve: Everything You Need to Know

Backflow Valve Inc., a leading provider of innovative plumbing solutions, has announced the launch of their latest product, the Backflow Prevention Valve. This new addition to their line of plumbing valves is designed to prevent the backflow of contaminated water into the clean water supply, ensuring the safety and purity of the water supply in residential, commercial, and industrial settings.The Backflow Prevention Valve is specially designed to meet the unique needs of modern plumbing systems, providing an effective and reliable solution for preventing cross-contamination and backflow events. The valve is engineered to meet the stringent standards set by the industry, providing peace of mind to homeowners, business owners, and facility managers who are concerned about the safety and integrity of their water supply."We are thrilled to introduce the Backflow Prevention Valve to our customers," said John Smith, CEO of Backflow Valve Inc. "This product represents our continued commitment to providing high-quality, reliable plumbing solutions that meet the evolving needs of our customers. With the increasing concern about water safety and contamination, our Backflow Prevention Valve offers a simple yet effective way to protect the purity of the water supply in any building or facility."The Backflow Prevention Valve features a durable construction and a user-friendly design, making it easy to install and maintain. It is available in a range of sizes to accommodate different plumbing systems and is compatible with various piping materials, making it a versatile solution for a wide range of applications.In addition to preventing backflow events, the Backflow Prevention Valve also helps to reduce the risk of costly water damage and potential health hazards associated with contaminated water. By providing a reliable barrier against backflow, the valve helps to safeguard the water supply and prevent the potential spread of harmful bacteria and other contaminants.The introduction of the Backflow Prevention Valve further solidifies Backflow Valve Inc.'s position as a trusted leader in the plumbing industry. With a strong focus on innovation and customer satisfaction, the company has built a reputation for delivering high-quality products that address the unique challenges faced by plumbing professionals and property owners.Backflow Valve Inc. has been at the forefront of the plumbing industry for over 20 years, continually developing and refining their product line to meet the changing needs of the market. Their team of experienced engineers and technicians work tirelessly to create cutting-edge solutions that offer superior performance, reliability, and ease of use."We take great pride in our ability to provide innovative, high-quality plumbing solutions that deliver true value to our customers," said Smith. "The Backflow Prevention Valve is a testament to our ongoing commitment to excellence and our dedication to ensuring the safety and reliability of plumbing systems in homes, businesses, and industrial facilities."As part of their commitment to customer satisfaction, Backflow Valve Inc. provides comprehensive support and training for their products, ensuring that plumbing professionals and property owners are equipped with the knowledge and resources they need to install and maintain their plumbing systems effectively.For more information about the Backflow Prevention Valve and other innovative products from Backflow Valve Inc., visit their website at www.backflowvalve.com or contact their customer service team. With their latest offering, Backflow Valve Inc. continues to set the standard for quality, reliability, and innovation in the plumbing industry.

Read More

Top Quality Union Ball Valve Suppliers for Reliable Industrial Solutions

**Rising Demand for Union Ball Valves Drives Market Growth: Industry Insights and Supplier Overview**The industrial valve sector is witnessing a significant surge in demand for union ball valves, a trend fueled by their essential role across various industries such as oil and gas, chemical processing, water treatment, and HVAC systems. These valves, known for their reliability and ease of maintenance, have become indispensable components in pipeline management and fluid control systems. As markets expand and industrial processes become more complex, suppliers of union ball valves are scaling operations to meet the increasing requirements of global clients.**Understanding the Union Ball Valve and Its Applications**A union ball valve is a type of quarter-turn valve that uses a hollow, perforated, and pivoting ball to control flow through it. The “union” feature indicates that the valve has a design that allows for easy disassembly and reassembly without disturbing the connected piping, making maintenance and replacement straightforward and cost-effective.Their design facilitates quick installation and minimal downtime, which is critical in industries where halting operations can have significant financial repercussions. Union ball valves are versatile, accommodating a range of fluids, temperatures, and pressures, which makes them suitable for applications from residential plumbing to large-scale industrial projects.**Market Drivers and Industry Trends**The increasing construction activities in emerging economies, along with the growth of sectors like petrochemicals and pharmaceuticals, have directly influenced the demand for high-quality industrial valves, including union ball valves. Moreover, the shift towards automation in fluid control systems has encouraged manufacturers to develop valves compatible with advanced control systems, enhancing operational efficiency and safety.Environmental regulations are also shaping the valve market by emphasizing leak-proof and corrosion-resistant components. Union ball valves made from advanced materials such as stainless steel and brass fulfill these criteria, providing durability and compliance with stringent standards.Another key trend is the customization of valves to suit specific operational parameters. Suppliers are now focusing on offering bespoke solutions, including size variations, actuator compatibility, and enhanced sealing technologies, to meet the nuanced needs of different industries.**Supplier Capabilities and Industry Contributions**Leading suppliers of union ball valves have demonstrated robust expertise in design, manufacturing, and quality assurance. Their offerings typically comply with international standards such as API, ISO, and ANSI, ensuring global compatibility and acceptance.Many suppliers maintain vertically integrated production facilities, allowing them to control every aspect of the valve manufacturing process—from raw material sourcing to final testing. This integration guarantees consistent quality and enables rapid response to market demands.In addition to product quality, value-added services such as technical support, custom engineering, and after-sales service distinguish top-tier suppliers. They collaborate closely with clients to optimize valve selection and system design, thus enhancing overall performance and lifecycle management.**Innovation and Sustainability Focus**Responding to evolving market needs, suppliers are investing heavily in research and development to produce union ball valves that accommodate high-pressure and high-temperature environments while minimizing environmental impact. Innovations include the development of valves with enhanced sealing systems that reduce fugitive emissions, contributing to sustainable operations.Furthermore, the adoption of digital technologies such as IoT-enabled valve monitoring systems is becoming commonplace. These smart valves provide real-time data on valve status, enabling predictive maintenance and reducing unplanned downtime.Sustainability initiatives also drive material selection and manufacturing processes. Eco-friendly coatings and recyclable materials are increasingly preferred, aligning with global efforts to reduce industrial carbon footprints.**Conclusion**The union ball valve market is poised for robust growth, driven by diversification of industrial applications, stringent regulatory landscapes, and technological advancements. Suppliers who combine product excellence with innovative solutions and comprehensive customer support are set to lead the industry.As industries continue to prioritize efficiency, safety, and sustainability, the role of reliable and adaptable valve components like the union ball valve becomes even more critical. Stakeholders within the supply chain should therefore consider the evolving trends and supplier capabilities when making procurement decisions, ensuring optimized performance and long-term value.With the ongoing commitment to quality, innovation, and environmental responsibility, union ball valve suppliers are not only meeting current industrial challenges but are also paving the way for future advancements in fluid control technology.

Read More

Find a Reliable One-Way Water Valve for Your Needs

One Way Water Valve Company Leads Innovation in Water Control TechnologyAs water scarcity becomes an increasingly pressing global issue, innovative solutions for controlling water flow and usage are in high demand. One company at the forefront of this technology is a leading manufacturer of one-way water valves, providing state-of-the-art solutions for water control and conservation.Founded over two decades ago, the company has been dedicated to developing and producing high-quality one-way water valves, designed to regulate the flow of water in various applications. These valves are renowned for their reliability, efficiency, and durability, making them an ideal choice for industrial, commercial, and residential use.The company's commitment to innovation has led to the development of a range of cutting-edge water valve technologies. Through ongoing research and development, they have continually improved their products, incorporating the latest advancements in materials and design to ensure optimal performance and longevity.One of the company's flagship products is the Automatic Water Shut-Off Valve, which has gained widespread acclaim for its ability to detect leaks and automatically shut off the water supply to prevent damage and wastage. This innovative valve is equipped with advanced sensors and control mechanisms, offering a seamless and reliable solution for water leak prevention.In addition to their focus on technological advancement, the company also places a strong emphasis on environmental responsibility. Their water valves are designed to promote water conservation and efficiency, helping users reduce their water consumption and minimize their environmental impact. By providing sustainable water control solutions, the company is contributing to global efforts to address water scarcity and promote the responsible use of natural resources.Furthermore, the company's commitment to quality and customer satisfaction sets them apart in the industry. With a dedication to excellence in manufacturing and customer service, they have established a strong reputation for reliability and integrity. Their clients range from small businesses to multinational corporations, all of whom benefit from the superior performance and reliability of their water valve products.Recently, the company announced the launch of a new line of smart water valves, incorporating cutting-edge technology to provide enhanced functionality and connectivity. These smart valves are equipped with IoT (Internet of Things) capabilities, allowing for remote monitoring and control of water flow through a mobile app or web interface. This advancement represents a significant leap forward in water control technology, offering users unprecedented convenience and control over their water systems.The company's ongoing commitment to innovation and sustainability has earned them recognition and accolades within the industry. They have been awarded several patents for their groundbreaking water valve technologies, and their products are widely regarded as the benchmark for quality and performance in the market.Looking ahead, the company has ambitious plans for further expansion and development, with a focus on new technological advancements and market growth. By continuing to push the boundaries of water control technology and sustainability, they aim to solidify their position as a global leader in the industry and contribute to a more water-secure and sustainable future for all.In conclusion, the One Way Water Valve Company stands at the forefront of innovation in water control technology, with a track record of excellence in product development and customer satisfaction. Their commitment to quality, sustainability, and technological advancement positions them as a trusted partner for businesses and individuals seeking reliable and efficient water valve solutions. As they continue to push the boundaries of what is possible in water control technology, the company is poised to make a significant impact on the global effort to address water scarcity and promote responsible water usage.

Read More

Top PVC Gate Valve Suppliers | Quality PVC Valve Providers

Certainly! Please provide the company introduction text you would like me to incorporate, and I will draft an 800-word news article about PVC gate valve suppliers with the brand name removed.

Read More

High-Quality Customized Lift Check Valves for All Your Needs

We are pleased to announce that a leading company in the valve industry has released a new and innovative product – the Custom Lift Check Valve. This valve is designed to provide reliable and efficient operation in a variety of industrial applications, and is set to be a game-changer in the field of fluid control systems.The Custom Lift Check Valve is designed to offer superior performance and reliability, making it an ideal choice for critical industrial processes where valve failure is not an option. This valve is capable of handling high pressure and high temperature conditions, making it suitable for use in a wide range of industries, including oil and gas, petrochemical, power generation, and more.One of the key features of the Custom Lift Check Valve is its customizability. This valve can be tailored to meet the specific requirements of each individual application, ensuring that it provides optimal performance and efficiency. This level of customization sets the Custom Lift Check Valve apart from other valves on the market, making it a highly desirable option for engineers and operators seeking the best possible solution for their fluid control needs.In addition to its customizability, the Custom Lift Check Valve also offers a number of other key benefits. It is designed to provide low pressure drop, which helps to minimize energy consumption and optimize system performance. The valve is also engineered for quick and easy installation and maintenance, saving time and resources for the end user.The company behind the Custom Lift Check Valve is a well-established leader in the valve industry, with a strong reputation for delivering high-quality products and exceptional customer service. With decades of experience and expertise in the field, the company is known for its commitment to innovation and continuous improvement, and the Custom Lift Check Valve is a prime example of this dedication to excellence.The company's state-of-the-art manufacturing facilities and rigorous quality control processes ensure that each Custom Lift Check Valve meets the highest standards for performance, reliability, and durability. By investing in the latest technologies and manufacturing techniques, the company is able to deliver cutting-edge products that are at the forefront of the industry.Furthermore, the company's team of engineers and technical experts are available to provide support and assistance to customers, helping them to select the right valve for their specific needs and offering guidance on installation, operation, and maintenance. This level of customer support sets the company apart from its competitors and ensures that customers receive the best possible experience when working with the company and its products.The release of the Custom Lift Check Valve represents a significant milestone for the company, further solidifying its position as a leading innovator in the valve industry. With its unparalleled customizability, superior performance, and exceptional support, the Custom Lift Check Valve is set to become the go-to choice for engineers and operators seeking the best possible solution for their fluid control needs.In conclusion, the Custom Lift Check Valve from the company is a groundbreaking new product that is poised to revolutionize the way industrial processes are controlled. With its customizability, high performance, and exceptional support, this valve is set to become the industry standard for reliability and efficiency. For more information about the Custom Lift Check Valve and the company behind it, please visit their website or contact their team directly.

Read More

Top Air Check Valve Manufacturer for Reliable Valve Solutions

Certainly! Please provide the specific news content and the company introduction you want me to use. Once I have those details, I can draft an 800-word news article for you without mentioning the brand name.

Read More

High-Quality Dual Check Valve Manufacturer for Reliable Industrial Solutions

Certainly! Please provide the company introduction you would like me to incorporate into the news article, and I will draft an 800-word news piece about the dual check valve manufacturer accordingly.

Read More