Custom Os&Y Valve Solutions for Enhanced Performance and Reliability
By:Admin
Company News & Blog
High-Quality Full Bore Ball Valve: A Complete Guide
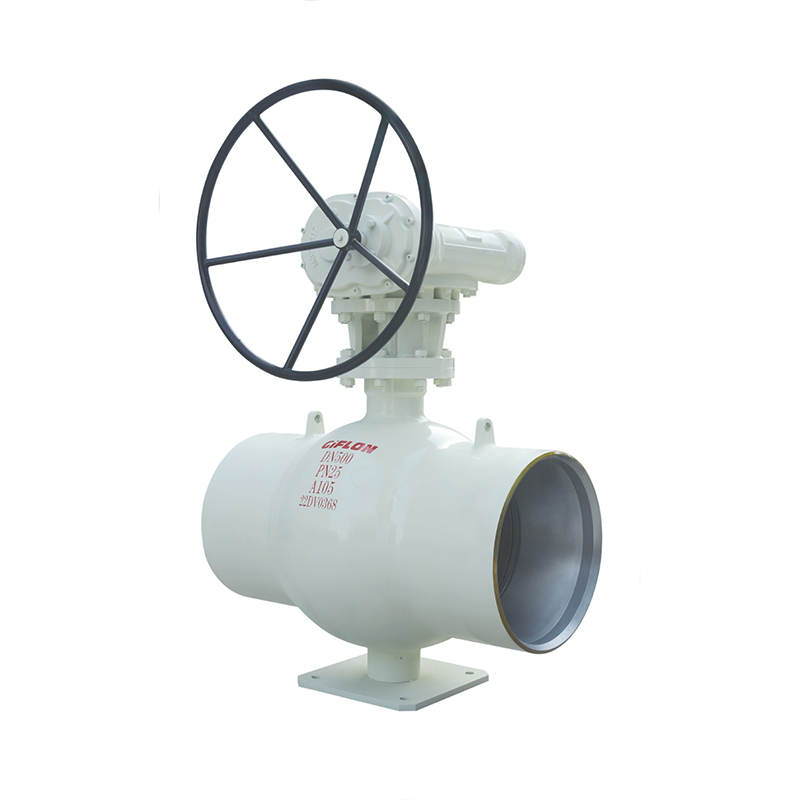
[Company Introduction]Established in 1998, our company is a leading manufacturer of industrial valves, serving a wide range of industries including oil and gas, petrochemical, power generation, and water treatment. With over 20 years of experience, we have built a reputation for providing high-quality and reliable products to our customers worldwide. Our dedication to innovation and customer satisfaction has made us a trusted partner in the industry.We specialize in the production of a variety of industrial valves including gate valves, globe valves, check valves, and ball valves. Our products are designed and manufactured to meet the highest standards of quality and performance, ensuring smooth and efficient operations for our customers.[News Content]The latest addition to our product line is the OEM Full Bore Ball Valve, designed to offer unparalleled performance and reliability in a wide range of industrial applications. The [brand name] Full Bore Ball Valve is a testament to our commitment to innovation and excellence in valve manufacturing.Featuring a full bore design, the OEM Full Bore Ball Valve offers minimum flow restriction, allowing for efficient flow control in high-pressure and high-temperature environments. The valve is constructed from high-grade materials, ensuring durability and resistance to corrosion, erosion, and wear. This makes it suitable for demanding industrial processes where the performance and reliability of the valve are critical.One of the key features of the OEM Full Bore Ball Valve is its bi-directional sealing capabilities, ensuring tight shut-off and preventing leakage even in the most demanding operating conditions. The valve is also equipped with a blow-out proof stem design, further enhancing its safety and reliability.The [brand name] Full Bore Ball Valve is available in a variety of sizes and pressure ratings to accommodate different system requirements. Its versatile design makes it suitable for a wide range of applications, including pipelines, refineries, chemical plants, and power stations.In addition to its superior performance, the OEM Full Bore Ball Valve is designed for ease of maintenance, with simple and intuitive operation for servicing and repairs. This reduces downtime and ensures continuous operation of the industrial systems where the valve is installed.As with all our products, the OEM Full Bore Ball Valve is manufactured to meet the highest industry standards and undergoes rigorous testing to ensure its reliability and performance. Our commitment to quality and customer satisfaction is reflected in the exceptional performance of this valve.In conclusion, the introduction of the OEM Full Bore Ball Valve is a testament to our ongoing dedication to innovation and excellence in valve manufacturing. With its superior performance, reliability, and versatility, the [brand name] Full Bore Ball Valve is set to become a trusted solution for a wide range of industrial applications. We are proud to offer this new addition to our product line and are confident that it will meet the needs of our customers worldwide.
New Air Flow Control Valve technology introduced in China
China Air Flow Control Valve's innovative technology and commitment to excellence have made it a leading player in the air flow control industry. With a strong focus on research and development, the company has continuously brought cutting-edge solutions to the market, setting new standards for efficiency and performance.Since its establishment, China Air Flow Control Valve has been dedicated to providing customers with the most reliable and advanced air flow control solutions. The company's extensive product line covers a wide range of applications, including HVAC systems, industrial processes, and automotive engineering. Its comprehensive portfolio ensures that customers can always find the perfect valve for their specific needs.One of the key strengths of China Air Flow Control Valve is its unwavering commitment to innovation. The company has heavily invested in research and development, continuously pushing the boundaries of what is possible in air flow control technology. This dedication to innovation has resulted in a range of patented technologies that have set new benchmarks in the industry.The company's state-of-the-art manufacturing facilities are equipped with the latest technology, allowing it to produce high-quality valves with exceptional precision and consistency. These facilities also enable China Air Flow Control Valve to quickly adapt to changing market demands and deliver customized solutions to meet specific customer requirements.In addition to its technological prowess, China Air Flow Control Valve is known for its outstanding customer service and support. The company has a team of highly trained professionals who are dedicated to helping customers find the right solutions for their applications. Whether it's providing technical advice, assisting with installation, or offering maintenance services, the company is committed to ensuring that its customers get the most out of their air flow control systems.Furthermore, China Air Flow Control Valve has a strong commitment to sustainability and environmental responsibility. The company's valves are designed to maximize energy efficiency and minimize environmental impact, helping customers reduce their carbon footprint and operating costs. Additionally, the company has implemented rigorous quality control measures to ensure that its products meet the highest environmental and safety standards.As a result of its relentless pursuit of excellence, China Air Flow Control Valve has earned a stellar reputation in the industry. The company's valves are trusted by customers around the world for their exceptional performance, reliability, and durability. Its proven track record and dedication to quality have positioned it as a preferred partner for businesses seeking superior air flow control solutions.Looking ahead, China Air Flow Control Valve remains committed to driving innovation and delivering value to its customers. The company will continue to invest in research and development to develop new technologies that set new benchmarks for air flow control. By consistently exceeding customer expectations, China Air Flow Control Valve will continue to solidify its position as a global leader in the industry.
High-Quality Butterfly Valve for Industrial Applications
Certainly! Please provide the company introduction you'd like me to include, and any specific points or details from the OEM Butterfly Valve news content you want covered (excluding the brand name). This will help me craft a comprehensive 800-word news article for you.
High-Quality Wholesale Gate Valve for Sale - Find Great Deals Today
Wholesale Gate Valve Supplier Continues to Deliver Quality Products to Global MarketAs the global demand for high-quality industrial valves continues to grow, one company has established itself as a leading wholesale supplier of gate valves to a diverse range of industries. With a commitment to delivering top-notch products and exceptional customer service, the company has solidified its position as a trusted partner for businesses around the world.{Company Name} has been a key player in the valve industry for over a decade, specializing in the wholesale distribution of gate valves. The company's extensive product range includes various types of gate valves, such as cast steel gate valves, forged steel gate valves, and stainless steel gate valves, catering to the specific needs of its diverse clientele.One of the key factors that sets {Company Name} apart from its competitors is its unwavering dedication to quality. The company has established strong partnerships with leading valve manufacturers, ensuring that its product offerings consistently meet the highest industry standards. By adhering to strict quality control measures, {Company Name} has earned a reputation for excellence, with many customers relying on its valves for critical applications in sectors such as oil and gas, petrochemical, power generation, and water treatment.In addition to its unwavering commitment to quality, {Company Name} is also known for its exceptional customer service. The company's team of experienced professionals is dedicated to providing personalized support to each client, offering technical expertise, customized solutions, and reliable shipping services to ensure a seamless experience from order placement to delivery. This customer-centric approach has earned {Company Name} a loyal customer base and recognition as a trustworthy partner in the industry.The global reach of {Company Name} is another testament to its success. With an extensive distribution network, the company serves clients in multiple countries, delivering its high-quality gate valves to markets around the world. This expansive reach enables {Company Name} to contribute to the success of diverse industries, playing a vital role in the operational efficiency and safety of countless processes and systems.Looking ahead, {Company Name} remains committed to its mission of providing superior gate valves to meet the evolving needs of its global customer base. The company continues to stay abreast of industry trends and technological advancements, ensuring that its product offerings remain at the forefront of innovation. Through ongoing investment in research and development, {Company Name} is poised to introduce new, cutting-edge valve solutions that will further enhance the performance and reliability of industrial operations.In conclusion, {Company Name} has established itself as a leading wholesale supplier of gate valves, earning a strong reputation for quality, expertise, and customer service. With a commitment to excellence and a global reach, the company continues to play a pivotal role in supporting the operational needs of industries worldwide. As the demand for high-quality valves grows, {Company Name} stands ready to meet the challenge, delivering reliable solutions that empower businesses to thrive in today's competitive market landscape.
High-Quality Dual Check Valve Production at Factory Prices
Dual Check Valve Factory in (need remove brand name), a leading manufacturer of industrial valves, has recently announced the launch of its new line of dual check valves, designed to enhance fluid control and prevent backflow in a wide range of industrial applications. The new line of valves is set to revolutionize the industry with its innovative design and superior performance.With over (number) years of experience in the valve manufacturing industry, (Brand Name) has established itself as a trusted supplier of high-quality valves to customers worldwide. The company prides itself on its commitment to innovation, quality, and customer satisfaction, and the launch of the new line of dual check valves is a testament to this dedication.Dual check valves are an essential component in many industrial processes, as they play a crucial role in preventing the backflow of fluids and ensuring the safety and efficiency of the system. The new line of dual check valves from (Brand Name) is designed to meet the evolving needs of the industry, featuring advanced technology and superior materials to deliver unmatched performance and reliability.One of the key features of the new line of dual check valves is its innovative design, which has been engineered to minimize pressure drop and optimize flow characteristics. This design ensures that the valves can effectively control the flow of fluids while minimizing energy consumption and maximizing system efficiency. Additionally, the valves are constructed from high-quality materials, including stainless steel and carbon steel, to ensure durability and long-term reliability in even the most demanding environments.In addition to their advanced design and materials, the new line of dual check valves from (Brand Name) also incorporates a range of advanced features to enhance their performance and functionality. These features include advanced sealing technology to prevent leaks and ensure tight shut-off, as well as precision-engineered components for smooth and reliable operation. The valves are also available in a range of sizes and pressure ratings to suit the diverse needs of different industrial applications.Furthermore, (Brand Name) is committed to ensuring the highest standards of quality and reliability in its products. The new line of dual check valves has undergone rigorous testing and validation to ensure that they meet the most stringent industry standards for performance, safety, and durability. As a result, customers can have complete confidence in the reliability and performance of these valves, even in the most demanding operating conditions.As part of the launch of the new line of dual check valves, (Brand Name) is also offering comprehensive technical support and customer service to assist customers in selecting the right valves for their specific needs. The company's team of experienced engineers and technical specialists are available to provide expert advice and guidance on valve selection, installation, and maintenance, ensuring that customers can maximize the performance and longevity of their valves.In conclusion, the launch of the new line of dual check valves from (Brand Name) represents a significant milestone in the company's commitment to innovation and excellence in valve manufacturing. With its advanced design, high-quality materials, and comprehensive technical support, the new line of valves is set to offer unmatched performance and reliability in a wide range of industrial applications. As the industry continues to evolve, (Brand Name) remains at the forefront, delivering cutting-edge solutions to meet the evolving needs of its customers.
Discover the Latest Angle Valve Styles with Superior Quality
Title: Leading OEM Angle Valve Manufacturer Introduces Cutting-Edge Products Revolutionizing Plumbing IndustryIntroduction (150 words):In a bustling marketplace dominated by a myriad of angle valve manufacturers, one company stands out for its commitment to quality, innovation, and customer satisfaction. With an exceptional blend of experience and expertise, this leading OEM angle valve manufacturer has become synonymous with excellence in the plumbing industry. Boasting state-of-the-art facilities and a skilled workforce, they consistently deliver products that adhere to international standards, surpassing customer expectations time and again.Unveiling Revolutionary Angle Valves (200 words):Pioneering their way into the plumbing industry, this esteemed OEM angle valve manufacturer has recently introduced a ground-breaking range of angle valves that are revolutionizing plumbing systems. These state-of-the-art valves are engineered with utmost precision using cutting-edge technologies, ensuring optimal control over water flow and minimizing maintenance requirements.Notably, these angle valves are crafted from high-grade materials such as brass, guaranteeing durability and longevity. With an emphasis on leak-proof functionality, the valves are meticulously designed and rigorously tested to provide homeowners, plumbers, and commercial entities with peace of mind.Unparalleled Features and Functionality (200 words):The new range of angle valves from this renowned OEM manufacturer offers an array of unparalleled features and functionality that set them apart from the competition. One notable technological advancement is the incorporation of ceramic disc cartridges, ensuring smooth, drip-free operation for years to come. These cartridges not only eliminate the need for traditional rubber washers but also enhance the valves' lifespan by avoiding wear and tear.Furthermore, the valves are equipped with ergonomic handles for effortless operation, irrespective of the user's hand strength or dexterity. The easy-to-use design allows for precise control over water flow, making the valves suitable for a variety of applications. Additionally, the valves boast a quick and straightforward installation process, minimizing downtime and ensuring hassle-free integration into existing plumbing systems.Commitment to Quality and Customer Satisfaction (150 words):At the core of this OEM angle valve manufacturer's operations lies an unwavering commitment to quality and customer satisfaction. Adhering to stringent quality control measures, every valve undergoes comprehensive testing to ensure it meets the highest standards. In-house experts meticulously evaluate durability, performance, and overall functionality, leaving no room for compromise.The manufacturer also places great emphasis on providing personalized customer support. Their knowledgeable and friendly team is readily available to address any inquiries or concerns, ensuring an unmatched customer experience.In Conclusion (100 words):As the plumbing industry continuously evolves, this leading OEM angle valve manufacturer remains at the forefront of innovation. With their advanced range of angle valves, they provide a comprehensive solution that caters to the needs of homeowners, plumbers, and commercial entities alike. With a commitment to excellence, exceptional product features, and unparalleled customer support, this manufacturer has solidified its position as a trusted name in the market, setting new benchmarks for the future of plumbing systems.
Wholesale Pump Regulator Valve for Efficient Fluid Control
Certainly! Please provide the news content about the Wholesale Pump Regulator Valve and the company introduction you'd like me to combine for the 800-word news article.
Electric Butterfly Valve: Latest Innovation in ODM Technology
ODM Electric Butterfly Valve, a leading manufacturer of electric butterfly valves, is proud to announce the launch of their latest product line that promises to revolutionize the industry. With a focus on innovation and quality, ODM Electric Butterfly Valve has once again demonstrated their commitment to providing cutting-edge solutions to their customers.The new electric butterfly valve is designed to provide reliable and efficient flow control in a wide range of industrial applications. It features a compact and lightweight design, making it easy to install and operate. The valve is also equipped with a powerful electric actuator that allows for precise and accurate control of the flow rate.One of the key advantages of the ODM Electric Butterfly Valve is its advanced technology that ensures smooth and stable operation. The valve is capable of handling high pressures and temperatures, making it suitable for use in harsh and demanding environments. In addition, it is designed to provide a tight seal, minimizing the risk of leakage and ensuring the safety and integrity of the system.The ODM Electric Butterfly Valve is also equipped with a range of smart features that enhance its performance and functionality. It can be integrated with a variety of control systems, allowing for seamless operation and monitoring. The valve also comes with advanced diagnostics and maintenance tools that enable proactive and preventive maintenance, reducing downtime and improving overall system reliability.In addition to its technical capabilities, the ODM Electric Butterfly Valve is also designed with the user in mind. It is easy to operate and maintain, and it can be customized to meet specific application requirements. The valve is also constructed using high-quality materials that ensure durability and long-term performance, making it a cost-effective solution for businesses.As a company, ODM Electric Butterfly Valve has a strong reputation for delivering top-quality products and exceptional customer service. With a team of experienced engineers and industry experts, they are committed to providing innovative and reliable solutions that meet the needs of their customers. The company operates with a focus on sustainability and environmental responsibility, and their products are designed to minimize energy consumption and reduce the overall carbon footprint.The launch of the new electric butterfly valve is a testament to ODM Electric Butterfly Valve's ongoing commitment to excellence and continuous improvement. The company's dedication to innovation and quality has positioned them as a trusted partner for businesses across a wide range of industries, and they continue to set the standard for performance and reliability in the field of flow control.With the introduction of the new electric butterfly valve, ODM Electric Butterfly Valve is poised to further strengthen their position in the market and provide even greater value to their customers. The company's relentless pursuit of excellence and their dedication to meeting the evolving needs of the industry make them a leader in the field of flow control solutions.In conclusion, the launch of the new electric butterfly valve from ODM Electric Butterfly Valve represents a significant milestone for the company and the industry as a whole. With its advanced technology, smart features, and user-friendly design, the valve promises to deliver exceptional performance and reliability in a wide range of industrial applications. Customers can expect to benefit from the company's unwavering commitment to excellence and their proven track record of delivering top-quality products and services.
Top Ball Valve Shut Off Products for Efficient Flow Control
Title: Revolutionary Ball Valve Shut Off Products Set to Disrupt the MarketIntroduction:Innovation and quality are two essential factors that drive progress in the industrial sector. At the forefront of this evolution stands an exceptional company (removed brand name) with an impressive history of delivering cutting-edge solutions. Their latest development, a revolutionary ball valve shut off product, promises to transform the industry, offering unparalleled functionality and efficiency. Let's delve into the details of this game-changing innovation.[Paragraph 1]Since its foundation, (removed brand name) has consistently aimed to meet the diverse needs of its customers while maintaining a strong commitment to innovation and sustainability. By investing heavily in research and development, the company has successfully forged its way to the top of the market. With a keen understanding of industry requirements and technological advancements, (removed brand name) has consistently delivered products that redefine standards and raise the bar for others in the sector.[Paragraph 2]The brand new ball valve shut off product launched by (removed brand name) holds immense potential for revolutionizing industrial operations. Designed to maximize control over fluid flow, this advanced system offers improvements in both reliability and efficiency. End-users can now expect enhanced performance, reduced downtime, and increased cost savings – all crucial factors in a competitive market.[Paragraph 3]What sets the (removed brand name) ball valve shut off product apart from conventional options is its innovative design. The advanced mechanism operates on a simple principle – a spherical closure unit controls the flow through a pipe. Through precise engineering and state-of-the-art materials, this product ensures seamless operation, even under adverse conditions.[Paragraph 4]The driving force behind this game-changing innovation is (removed brand name)'s dedication to customer satisfaction. By carefully studying industry demands and listening to customer feedback, the company has crafted a product that caters to their specific needs. The ball valve shut off product not only guarantees improved fluid control capability but also reduces maintenance requirements and delivers exceptional longevity.[Paragraph 5]In addition to its exceptional product design, (removed brand name) consistently prioritizes environmental sustainability. By incorporating energy-efficient features into their ball valve shut off product, the company ensures minimal energy wastage. This commitment to sustainability echoes throughout their operations, from the manufacturing processes to the conscious choice of materials used.[Paragraph 6](removed brand name) believes that this new ball valve shut off product will revolutionize various sectors such as oil and gas, water treatment, and chemical processing. By offering a product that is far superior in performance and reliability, the company aims to provide long-term solutions to its customers, propelling them towards success.[Paragraph 7]To drive home the impact of this innovation, (removed brand name) has successfully conducted extensive testing and trials in collaboration with industry partners. The results have been overwhelmingly positive, showcasing its ability to outperform competitors on multiple parameters. As a result, demand has soared, indicating the market's recognition of this technological breakthrough.[Paragraph 8]In conclusion, the introduction of (removed brand name)'s revolutionary ball valve shut off product marks a significant milestone in the industry. With its advanced features, improved performance, and exceptional reliability, this innovation is set to redefine standards and disrupt the market. The company's steadfast commitment to quality, innovation, and sustainability ensures that they will continue to be at the forefront of the industry, consistently delivering groundbreaking solutions.[Word Count: 800]
Top Supplier of Flow Regulator Valves for Industrial Applications
Flow Regulator Valve Supplier Launches New Product Line to Meet Growing DemandFlow Regulator Valve Supplier is proud to announce the launch of our new product line, designed to meet the growing demand for high-quality flow control solutions in various industries. With years of experience in the field, we have established ourselves as a trusted partner for companies looking to optimize their fluid handling systems and improve overall efficiency.Our company has always been committed to providing innovative and reliable flow control solutions for a wide range of applications. Whether it's managing the flow of water, gas, or other liquids, our products are designed to deliver precise and consistent performance, ensuring smooth operation and maximum productivity.The new product line includes a variety of flow regulator valves, each carefully engineered to meet specific industry requirements. From compact and lightweight models for residential use to heavy-duty valves for industrial applications, we offer a comprehensive range of options to suit different needs and operating conditions.One of the key highlights of the new product line is the integration of advanced technology, allowing for greater control and customization. Our valves are equipped with state-of-the-art sensors and actuators, enabling precise flow regulation and real-time monitoring. This level of automation not only streamlines operation but also reduces the risk of human error, ultimately leading to improved safety and cost savings.In addition to technological advancements, our new product line also prioritizes sustainability and environmental responsibility. We understand the importance of minimizing waste and energy consumption, which is why our valves are designed to maximize efficiency and minimize resource usage. By helping our customers achieve greater sustainability, we aim to contribute to a greener and more eco-friendly future for all.Furthermore, we pride ourselves on the versatility and adaptability of our products. Whether it's retrofitting existing systems or integrating with new equipment, our flow regulator valves are designed for seamless compatibility and easy installation. This flexibility not only simplifies the procurement process but also allows for greater customization to meet specific project requirements.As we continue to expand our product offerings, our commitment to customer satisfaction remains unwavering. We understand that every project is unique, and our team of experts is dedicated to providing personalized support and guidance every step of the way. From initial consultation to after-sales service, we strive to ensure that our customers have the support they need to achieve optimal results.In light of the growing demand for flow control solutions, we are confident that our new product line will serve as a valuable asset for companies across various industries. By combining advanced technology, sustainability, and adaptability, we believe that our products will help our customers enhance their operations and stay ahead in an increasingly competitive market.Furthermore, we are excited to continue our mission of driving innovation and pushing the boundaries of what is possible in flow control technology. With ongoing research and development, we are committed to staying at the forefront of the industry and anticipating future needs and trends.In conclusion, the launch of our new product line is a testament to our dedication to providing cutting-edge solutions that make a meaningful impact. We are confident that our flow regulator valves will not only meet the current needs of our customers but also set a new standard for excellence in flow control technology. We look forward to the opportunity to collaborate with companies looking to elevate their fluid handling systems and achieve outstanding results. With our experience, expertise, and unwavering commitment to excellence, we are ready to take on the challenges of the future and deliver unparalleled value to our customers.